What Is the Best Rigid Flex PCB Manufacturer in China?

Choosing the best rigid flex pcb manufacturer in China requires more than comparing prices or factory photographs. Reliability depends on engineering discipline, material control, process validation, and transparent communication. A supplier may offer an attractive quotation. That does not prove production stability.

Industry data supports careful evaluation. Prismark’s 2024 PCB Industry Results and Forecast Report describes continued demand for advanced circuit technologies, driven by automotive electronics, medical devices, communications, and high-density consumer products. These applications require thinner structures, tighter bend controls, and more dependable interconnections. The 2024 IPC Global Electronics Manufacturing Services Statistical Series also highlights the importance of quality systems, supply-chain performance, and manufacturing capability when assessing electronics partners. Standards matter.

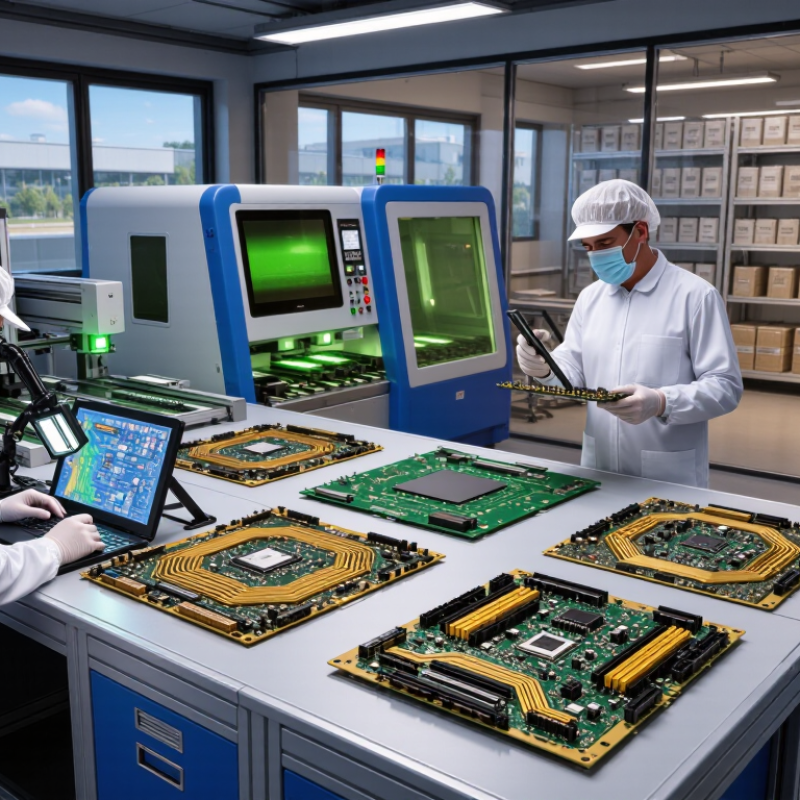
A strong Chinese manufacturer should demonstrate experience with polyimide materials, controlled impedance, laser drilling, coverlay alignment, stiffener bonding, and repeated flex testing. Ask for measurable evidence. Useful records include first-pass yield, customer complaint rates, audit results, microsection reports, and traceability samples. Certifications such as ISO 9001, IATF 16949, or ISO 13485 may be relevant, depending on the product’s market.

The best choice is not always the largest factory. It is the supplier that understands your design risks and explains them clearly. Factory scale can hide weak engineering support. A beautiful sample can also conceal inconsistent volume production. Request pilot builds, inspect cross-sections, and confirm testing methods before signing a long-term agreement. This guide compares Chinese rigid flex pcb manufacturers through technical expertise, quality evidence, production capacity, delivery reliability, and practical customer support. No ranking is flawless. Your application, tolerance limits, and risk profile must shape the final decision.
What Is the Best Rigid Flex PCB Manufacturer in China?

What Defines a Rigid-Flex PCB Under IPC-2223 and IPC-6013?

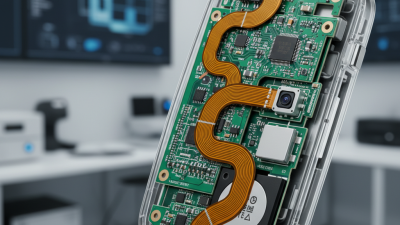
A rigid-flex PCB combines rigid board sections with flexible circuitry in one integrated construction. Under IPC-2223, its design must address both mechanical movement and electrical performance. It is not simply a flexible tail attached to a rigid board. The transition zone, bend area, layer stack-up, and support materials all influence reliability.

In practical production, the bend radius needs careful control. A sharp fold can crack copper or damage the dielectric. Designers usually define bending direction, minimum radius, and the number of flexing cycles. Coverlay openings, stiffeners, plated holes, and impedance requirements also need clear documentation. Small details matter.

IPC-6013 focuses on qualification and performance requirements for flexible and rigid-flex printed boards. A capable Chinese manufacturer should demonstrate controlled lamination, reliable plating, clean registration, and traceable inspection records. Microsection analysis can reveal voids, thin copper, or poor hole quality. Thermal cycling and flex testing add useful evidence.

Still, compliance is not automatic. A certificate alone may hide weak process control. I would review sample data, stack-up drawings, first-article reports, and failure analysis methods. Some designs look acceptable but fail near the rigid-flex transition. That area deserves extra attention. Standards also change, so the applicable IPC editions and customer requirements should be confirmed before production.
How Do Layer Count, Bend Radius, and 0.1-mm Traces Affect Performance?

What Is the Best Rigid-Flex PCB Manufacturer in China?

Layer count, bend radius, and 0.1-mm traces often decide rigid-flex PCB performance. A higher layer count can improve routing density, but it also increases stiffness and registration risk. More layers may restrict folding near transitions. The best manufacturer should provide stackup drawings, impedance data, and microsection evidence before production. A capability chart alone is not enough.

Bend radius must match the actual copper structure. Dynamic folding needs a larger radius than one-time installation. Thin copper, staggered vias, and carefully placed coverlay can reduce mechanical stress. Sharp corners remain a common failure point. In design reviews, I check the neutral axis, copper distribution, and the distance between rigid and flexible zones. These details are easy to overlook.

A 0.1-mm trace demands stable imaging, etching, and inspection control. Over-etching can narrow the line, while under-etching can affect spacing and impedance. The supplier should measure trace width on test coupons and record process variation. I would also request bend-cycle results using the finished stackup, not a simplified sample. My first assumption used to be that thinner traces always improved flexibility. That was incomplete. Copper thickness, adhesive flow, plating, and layer balance matter just as much. A reliable Chinese manufacturer should explain these trade-offs clearly and accept design changes when test results challenge the original plan.

Which Chinese Manufacturers Meet ISO 9001, UL, and IPC Class 2/3?

What Is the Best Rigid Flex PCB Manufacturer in China?

The stronger question is which Chinese manufacturer can prove consistent compliance. A reliable supplier should maintain ISO 9001 across design review, purchasing, fabrication, and final inspection. Ask for the current certificate, issuing body, validity dates, and covered site. One certificate may not cover every production location.

UL evidence needs careful checking. UL approval may apply to laminate, coverlay, or a specific construction, rather than the entire factory. Request certificate numbers, material ratings, and applicable thickness ranges. Do not assume. The details matter when a rigid-flex board combines polyimide layers, stiffeners, plated holes, and adhesive systems.

IPC Class 2 or Class 3 is normally demonstrated through controlled workmanship and inspection records. Ask how the factory manages conductor spacing, annular rings, flex-to-rigid transitions, solderability, and bend-radius limits. Useful records include microsection reports, impedance results, cleanliness tests, and first-article inspection data. A capable engineering team should explain stackup changes before production, not after failures appear. Ask for traceability from raw materials to finished panels.

Factory audits reveal practical discipline. Check humidity control, laser or mechanical drilling accuracy, coverlay registration, and sample storage. Also review nonconformance reports. A supplier showing only perfect results may be hiding useful lessons. In my experience, honest corrective-action records often provide stronger evidence than polished presentations. Some manufacturers meet the paperwork requirements but struggle with repeatability on dense, high-layer-count designs. Small pilot runs expose that weakness quickly.

How Do AOI, X-Ray Inspection, and 100% Electrical Testing Compare?

Choosing the best rigid-flex PCB manufacturer in China requires more than comparing prices. Inspection depth matters. AOI uses cameras to detect solder bridges, missing parts, misalignment, and visible conductor damage. It is fast and suitable for high-volume screening. However, cameras cannot reliably see buried vias, inner-layer shorts, or voids beneath components.

X-ray inspection reveals hidden structures. It can identify barrel voids, poor solder coverage, layer registration problems, and concealed delamination. The IPC-6013E performance specification emphasizes controlled construction and qualification for rigid-flex boards, but it does not make X-ray mandatory for every design. That decision depends on layer count, via structure, and reliability requirements. X-ray is powerful, though slower and more costly. Images also require experienced interpretation.

100% electrical testing checks every accessible net for continuity and isolation. It can detect open circuits that visual inspection misses. It does not prove solder quality or reveal internal voids. A strong supplier therefore combines all three methods, rather than treating one pass result as proof. IPC’s 2024 Electronics Industry Sentiment Report continues to identify quality consistency and manufacturing capacity as major industry concerns. The 2024 Prismark PCB market analysis also reports continued growth in advanced, high-density board applications, increasing inspection pressure.

Ask for defect-per-million data, false-call rates, calibration records, and sample inspection images. Request traceability from panel number to test result. A weakness remains: 100% testing can still miss intermittent faults. Good manufacturers admit that limitation and add thermal cycling or cross-section analysis when the application demands it.

What Is the Best Rigid Flex PCB Manufacturer in China? — How Do AOI, X-Ray Inspection, and 100% Electrical Testing Compare?
Inspection Method Primary Inspection Principle Defects or Conditions Detected Best Application in Rigid-Flex PCB Production Coverage Typical Throughput Main Limitations Recommended Use
Automated Optical Inspection (AOI) Uses cameras, lighting, image processing, and programmed design data to compare the manufactured circuit pattern with the intended pattern. Open circuits, shorts, missing or shifted components, incorrect conductor width, insufficient etching, copper bridging, pad damage, and visible registration errors. External copper layers, exposed pads, fine-pitch features, solder-mask alignment, coverlay registration, and visible flexible-area features. High for visible surfaces
Limited for hidden or internal structures.
High
Suitable for automated in-line or near-line inspection of repeated panels.
Cannot reliably verify concealed vias, internal-layer defects, voids, or electrical continuity. Results depend on lighting, image quality, programming, and surface contrast. Use after imaging and etching, and again when external-layer or coverlay alignment verification is required.
X-Ray Inspection Uses X-rays to create images based on differences in material density and thickness, allowing inspection through non-transparent PCB structures. Hidden voids, insufficient solder, concealed solder joints, internal-layer misregistration, via barrel conditions, buried features, and some delamination or foreign-material indications. Multilayer rigid-flex constructions, microvias, buried vias, blind vias, dense interconnects, and areas hidden beneath components or cover materials. High for internal and concealed features
Not a complete substitute for electrical testing.
Medium to low
Usually slower than AOI because image acquisition and interpretation require more time.
May not identify every open or short circuit. Image interpretation can be complex, and equipment cost, radiation controls, and process setup requirements are higher. Use for complex multilayer designs, high-density interconnects, hidden solder joints, and failure analysis of internal structures.
100% Electrical Testing Applies controlled test signals to verify electrical continuity, isolation, resistance, and, where specified, circuit functionality. Open circuits, shorts, incorrect connections, missing connections, net-to-net isolation failures, and certain resistance-related defects. Final verification of every tested net on rigid-flex circuits before shipment, especially for safety-critical or high-reliability assemblies. 100% of programmed test points or nets
Coverage depends on fixture access, test-point design, and the selected test method.
Medium to high
Fast for established high-volume products; initial setup may be longer for new designs.
Does not directly reveal cosmetic defects, conductor-shape variation, internal voids, or mechanical damage that does not affect the tested electrical path. Use as the final electrical acceptance step, combined with AOI and X-ray where visual or internal structural risks exist.
Flying-Probe Electrical Testing Uses movable probes to contact designated test points without requiring a dedicated permanent fixture. Open circuits, shorts, continuity failures, isolation failures, and selected resistance abnormalities. Prototype, low-volume, high-mix, or frequently revised rigid-flex PCB designs. High for accessible programmed points Low to medium
Testing is generally slower than a dedicated fixture at high production volumes.
Probe access can be difficult on very dense, small, curved, or heavily covered flexible areas. Mechanical probing may require suitable support and controlled contact force. Use for prototypes and small batches when avoiding dedicated fixture costs is important.
Fixture-Based Electrical Testing Uses a custom test fixture with multiple contacts to test many designated points in a repeatable sequence. Open circuits, shorts, incorrect net connections, isolation failures, and selected resistance defects. Stable, repeatable production of medium- and high-volume rigid-flex PCB designs. High for designed test coverage High
Efficient for repeat orders after fixture qualification.
Requires fixture design, manufacturing, maintenance, and proper support of flexible sections. Fixture coverage is limited to accessible and programmed test points. Use for high-volume production where fast and repeatable 100% electrical testing is required.
How to Evaluate a Rigid-Flex PCB Manufacturer
Inspection Capability The manufacturer should be able to match inspection methods to the construction, risk level, layer count, via technology, and assembly requirements of the design. Confirm the availability of AOI, X-ray inspection, and 100% electrical testing where applicable. Essential Ask whether inspection is performed in-line, by batch, or only on a sample basis. A single inspection method cannot detect every defect category in a rigid-flex PCB. Prefer a documented combination of optical, internal-structure, and electrical controls.
Process Traceability Production records should connect materials, process parameters, inspection results, operators, equipment, and shipment data to the relevant lot or panel. Useful for investigating recurring defects, customer complaints, and changes in yield. Essential Traceability is typically maintained throughout the production cycle rather than measured as inspection speed. Traceability alone does not prevent defects; it supports containment and corrective action. Request sample inspection records and a clearly defined lot-identification system.
Material and Dimensional Control Verifies laminate, copper, coverlay, adhesive, stiffener, finished thickness, bend-area dimensions, hole sizes, and layer registration against approved specifications. Critical for controlled impedance, repeated bending, connector fit, assembly compatibility, and mechanical reliability. Essential Usually performed at incoming, in-process, and final inspection stages. Dimensional inspection cannot prove electrical continuity or reveal all hidden internal defects. Ensure the manufacturer uses controlled drawings, approved material lists, and measurable acceptance criteria.
Recommended Inspection Combination AOI identifies visible pattern and alignment defects; X-ray examines concealed structures; 100% electrical testing verifies circuit connectivity and isolation. Most suitable for complex multilayer rigid-flex PCBs, fine-pitch designs, high-reliability products, and applications where field failure is costly. Broadest practical coverage Overall cycle time and cost are higher than using one method alone, but defect escape risk is reduced. Inspection plans must be designed around the actual PCB stack-up, test access, volume, and reliability requirements. For supplier selection, prioritize documented process control and complementary inspection coverage rather than relying on one “best” test.

Which Supplier Delivers the Best Balance of Cost, Lead Time, and Reliability?

What Is the Best Rigid Flex PCB Manufacturer in China?

The best supplier is not always the one offering the lowest quotation. A reliable choice balances cost, lead time, and consistent performance. In practical sourcing, I compare the full production path, not just the first price. A lower quote may exclude tooling, testing, engineering changes, or protective packaging. That difference can appear later as delay.

During supplier evaluation, request samples, process records, and recent delivery data. Check impedance control, layer alignment, bend performance, and solderability. Ask whether the factory performs microsection analysis, AOI, and electrical testing. Traceability also matters. Each panel should connect to materials, operators, inspection results, and shipment records. A realistic lead time includes design review, material preparation, fabrication, testing, and rework allowance. Very short promises deserve careful questions. They may be possible, but not always repeatable.

Tips: Compare three written quotations using the same stack-up and testing requirements. Ask for a pilot order before placing volume production. Confirm capacity during peak seasons. My own mistake was trusting an attractive price without checking engineering response time. The order arrived late, and the savings disappeared. Reliability often comes from ordinary details: clear drawings, controlled revisions, stable materials, and fast communication. A supplier that admits a process limitation can be safer than one promising everything.