China Best PCB Board Design Services for Global Buyers

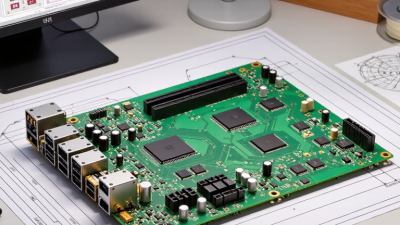
Global buyers evaluating China’s pcb board design services need more than a competitive quote. They need a design partner who can turn electrical requirements into a manufacturable, testable board. Component availability, layer stack-up, controlled impedance, thermal performance, and assembly limits all shape the result. A small oversight can mean a rerouted trace, a delayed prototype, or a board that fails testing.

Signal-integrity expert Dr. Eric Bogatin’s work emphasizes designing for the behavior of real interconnects, not treating traces as ideal wires. A concise editorial takeaway is: “A reliable board begins with understanding how its signals travel.” This is a paraphrase, not a verbatim quotation. It captures why early engineering review matters. Ask suppliers how they check high-speed paths, document design decisions, and handle revisions. Request concrete examples, such as impedance notes, stack-up proposals, and design-for-manufacturing feedback. Details matter.

This guide examines how global buyers can compare China-based design services, assess engineering communication, and reduce avoidable redesigns. It also considers the handoff from schematic and layout to fabrication and assembly. A polished portfolio is useful, but it cannot prove every claim. Verify capabilities against your board’s requirements, and clarify deliverables before work begins. No checklist removes all risk. Good questions help.
China Best PCB Board Design Services for Global Buyers

PCB Design Scope: From Schematic Capture to IPC-2221-Compliant Layout

China Best PCB Board Design Services for Global Buyers

Reliable PCB design begins with accurate schematic capture. Engineers review symbols, net names, power paths, and component footprints before placing parts. This early check prevents hidden connections and costly layout changes. Design teams also confirm voltage limits, current demand, signal direction, and manufacturing goals. Details matter. A missing return path can create noise, heat, or failed testing.

The layout process follows the approved schematic and a controlled layer stackup. Engineers separate sensitive analog traces from switching nodes and keep high-current paths short. They calculate clearance, creepage, trace width, copper weight, and thermal relief requirements. Each decision supports IPC-2221-compliant layout practices. Controlled impedance may also require specific dielectric thickness and routing geometry. These details should be recorded, not assumed.

Practical reviews improve reliability. Designers run design-rule checks, inspect drill locations, and compare the layout against fabrication limits. They also review assembly access, soldering clearances, and test-point placement. A clean report helps global buyers understand what was verified. Yet no layout is perfect. Component substitutions, incomplete drawings, or late mechanical changes can still create risk. Sometimes, the first review reveals a better solution. That is useful, not embarrassing. Careful teams document the change, update the files, and repeat the checks before release. The final package should include schematics, source layout data, fabrication drawings, assembly notes, and revision history.
PCB Board Design Scope: From Schematic Capture to IPC-2221-Compliant Layout

This reference workflow shows the typical engineering deliverables produced during a professional PCB design project. IPC-2221 is used as a generic design standard for safety, spacing, conductor geometry, materials, and reliability considerations.

The values represent the number of core design outputs commonly reviewed at each stage and are intended as a practical workflow reference rather than company-specific performance data.

Layer Counts, 3–6 mil Traces, and HDI Microvias for Global Applications

China Best PCB Board Design Services for Global Buyers

Layer selection must follow current, voltage, heat, and assembly limits. A six-layer board can separate power and signals more effectively than a four-layer design. However, extra layers also increase drilling, lamination, and inspection costs. The 2023 IPC Technology Roadmap identifies finer geometries and microvias as important directions for high-density electronics. In practical production, 3–6 mil traces support compact modules, but 3 mil routing demands tighter imaging control and cleaner fabrication.

HDI microvias can connect outer layers with short vertical transitions. They reduce via blockage and improve routing around processors, sensors, and wireless circuits. Industry market reports published in 2024 forecast HDI demand to grow at roughly 6% annually through 2030. That growth reflects smaller devices, not unlimited design freedom. A 3 mil trace is not automatically better. It may increase yield risk, inspection time, and rework exposure. This is where design experience matters. Small mistakes become expensive.

Tips: Match trace width with copper weight, dielectric thickness, and supplier capability. Ask for controlled-impedance data before layout approval. Confirm microvia stacking, aspect ratio, and reliability testing early. Use IPC-2221 guidance, but do not treat it as a complete manufacturing guarantee. A design can meet a drawing and still perform poorly after thermal cycling. Build a fabrication review into the process. It often reveals assumptions nobody questioned.

DFM Review: 0.10 mm Spacing, IPC-6012 Class 2/3, and Yield Control

A 0.10 mm spacing target can work, but it leaves little room for process variation. A useful DFM review checks minimum trace spacing against copper weight, layer position, and the fabricator’s etching capability. It should also inspect drill-to-copper clearance, annular rings, and solder mask registration. Small details matter. A clearance that looks adequate in CAD may shrink after etching or registration tolerances are applied.

IPC-6012 Class 2 and Class 3 represent different acceptance expectations, so the required class should be stated before production. Class 3 designs may need tighter attention to workmanship and inspection criteria, depending on the product requirements. Confirm the applicable revision, acceptance conditions, and any customer-specific notes with the fabricator. The class alone does not guarantee a particular field life. That distinction is easy to overlook.

Yield control starts with measurable checks, not optimistic promises. Compare the submitted Gerber data with the approved stackup, then review test coupons and first-article results where appropriate. Track recurring defects, such as shorts near fine-pitch pads or insufficient annular rings, and feed them back into the next layout revision. A wider spacing may improve robustness, but it can also force a larger board. There is no perfect rule; the trade-off deserves a real review.

China Best PCB Board Design Services for Global Buyers - DFM Review: 0.10 mm Spacing, IPC-6012 Class 2/3, and Yield Control
DFM Review Dimension Engineering Requirement or Target Applicable Standard / Reference Verification Method Typical Risk if Not Controlled Recommended Status
Minimum copper spacing 0.10 mm minimum spacing may be considered for selected high-density designs only after stack-up, copper weight, etching capability, and fabrication limits are confirmed. IPC-2221 design guidance; fabricator capability confirmation required Pre-production DFM rule check and fabrication capability review Electrical shorts, reduced etch margin, and lower production yield Engineering Review
Minimum trace width Trace width should be selected according to copper thickness, current demand, impedance requirements, and the manufacturer’s process window. IPC-2221 and IPC-2152 for design and current-carrying considerations CAD rule validation, current analysis, and cross-section review Overheating, impedance deviation, or open circuits after etching Design Target
Board acceptance class Class 2 is commonly used for dedicated-service electronic products; Class 3 is intended for high-reliability products where continued performance is essential. IPC-6012, rigid printed boards Purchase-order requirements, inspection plan, and qualification records Unclear acceptance criteria, disputes, and inconsistent inspection results Standard Defined
Finished board thickness Nominal thickness and tolerance should be specified with the layer count, dielectric construction, copper weight, and final surface finish. IPC-6012 and approved fabrication drawing Micrometer measurement at defined locations Mechanical fit problems, connector mismatch, or altered impedance Design Target
Plated through-hole quality Hole size, plating thickness, aspect ratio, and annular ring requirements should be defined before release to production. IPC-6012; inspection criteria should match the selected class Microsection analysis, dimensional inspection, and continuity testing Barrel cracks, poor solderability, intermittent connections, or opens Standard Defined
Via and annular ring design Finished hole diameter, pad diameter, registration tolerance, and via-to-copper clearance should be checked together. IPC-2221 and fabrication drawing requirements Automated optical inspection and dimensional capability study Breakout, insufficient plating land, or drill-to-pad registration defects Engineering Review
Controlled impedance Target impedance, tolerance, reference planes, dielectric thickness, copper roughness, and routing geometry should be documented. IPC-2141 guidance and project-specific signal-integrity requirements Stack-up calculation, test coupon measurement, and TDR testing when required Signal reflection, timing errors, crosstalk, and failed high-speed testing Design Target
Solder mask registration Pad expansion and mask clearance should accommodate registration tolerance without exposing unintended copper. IPC-6012 and approved solder-mask capability limits Artwork review and automated optical inspection Solder bridges, exposed conductors, or reduced insulation reliability Engineering Review
Surface finish selection Finish selection should consider shelf life, soldering process, contact requirements, wire bonding, and RoHS-related material restrictions. IPC-4552 series and project environmental requirements Material certification, thickness testing, and solderability evaluation Oxidation, poor wetting, contact wear, or assembly defects Standard Defined
Electrical test coverage Netlist-based open-and-short testing should be defined for production, with fixture or flying-probe selection based on volume and complexity. Customer test specification and IPC-9252 guidance where applicable Electrical test against the approved netlist Undetected opens, shorts, or latent functional failures Design Target
Automated optical inspection Inspection coverage should include solder-mask defects, copper pattern variation, missing features, and registration errors. Internal inspection plan aligned with IPC acceptance criteria AOI followed by manual review of flagged conditions Pattern defects reaching assembly or causing rework Design Target
Yield monitoring Track first-pass yield, defect Pareto, scrap rate, rework rate, and lot-to-lot variation; investigate recurring defects using corrective-action records. Process-control plan and customer quality agreement Statistical process control, defect records, and lot review Hidden process drift, rising cost, late delivery, and unstable quality Process Control
Thermal reliability Material system, copper distribution, plated-hole construction, and thermal cycling requirements should match the expected operating environment. IPC-6012 qualification requirements and project reliability specification Thermal cycling, solder float, or qualification testing as applicable Delamination, barrel cracking, pad lifting, or field failure Qualification Review
Documentation package Release data should include Gerber or ODB++ files, drill data, stack-up, fabrication drawing, test requirements, material requirements, and revision control. Customer-controlled engineering documentation Pre-production document checklist and revision comparison Wrong revision, ambiguous requirements, or production delays Release Controlled
Final acceptance Define visual, dimensional, electrical, solderability, cleanliness, packaging, and certificate requirements before mass production. IPC-6012, IPC-A-600, and purchase-order acceptance criteria Final inspection report, sampling plan, and certificate review Shipment rejection, inconsistent quality judgments, or customer claims Acceptance Defined
Note: The values shown are engineering planning references rather than universal manufacturing guarantees. Final limits should be confirmed against the approved stack-up, material system, fabrication drawing, applicable IPC class, and the selected manufacturing process.

Global Compliance: RoHS, REACH, UL 94 V-0, and 100 Ω Differential Pairs

Reliable PCB board design for global buyers begins with compliance built into the layout, not added at the end. Experienced Chinese engineering teams can review material declarations, stack-ups, creepage distances, and manufacturing limits before release. RoHS supports restricted-substance control, while REACH documentation helps clarify chemical requirements across supply chains. These records should match the actual laminate, solder mask, and surface finish. A missing document can delay production.

Signal integrity also needs practical attention. For 100 Ω differential pairs, designers should control trace width, spacing, dielectric thickness, and reference-plane continuity. Shorter routes are not always better. Unexpected vias, sharp geometry, or split planes may increase impedance variation.

Simulation helps, but test coupons provide stronger evidence during fabrication. UL 94 V-0 material selection can improve flame-resistance performance, yet the complete stack-up and assembly process still require verification. Mistakes happen.

Tips: Request a compliance matrix with every quotation. Ask for impedance coupons and cross-section reports. Confirm whether the quoted tolerance suits your interface speed. Keep revision control strict, especially when materials change. A thoughtful design review may reveal that one “approved” assumption was never properly measured. That small correction can protect yield, certification readiness, and field reliability.

Supplier Selection: ISO 9001, CAM Checks, Prototypes, and NPI Support

Choosing a PCB design supplier requires more than comparing quotations.

Global buyers need evidence of controlled processes and practical engineering experience. ISO 9001 certification can indicate documented procedures, traceability, and corrective action systems. However, certification alone does not guarantee strong board design results.

Ask how the supplier performs CAM checks before fabrication.

Engineers should review clearances, drill sizes, copper spacing, solder mask openings, and manufacturing limits. Request a design-for-manufacturing report with specific findings.

Prototype support is equally important.

A reliable team can produce sample boards, inspect assembly details, and record changes between revisions. Small issues often appear only after the first physical build.

Tips:

Review a sample inspection report. Confirm layer-stack expertise. Ask about impedance control. Check prototype lead times. Discuss secure file handling. For NPI, clarify ownership of the bill of materials, test fixtures, assembly instructions, and engineering change notices. Regular technical meetings can prevent expensive misunderstandings across time zones.

Still, no process is perfect. A supplier may pass every audit yet miss a thermal concern during layout. Buyers should therefore test communication through a small prototype project.

Measure response quality, documentation accuracy, and willingness to question unclear requirements. Honest feedback is more useful than confident promises.